
Virgilio Perez Guembe
Salesregion: South & Middle America, Europe, Asia
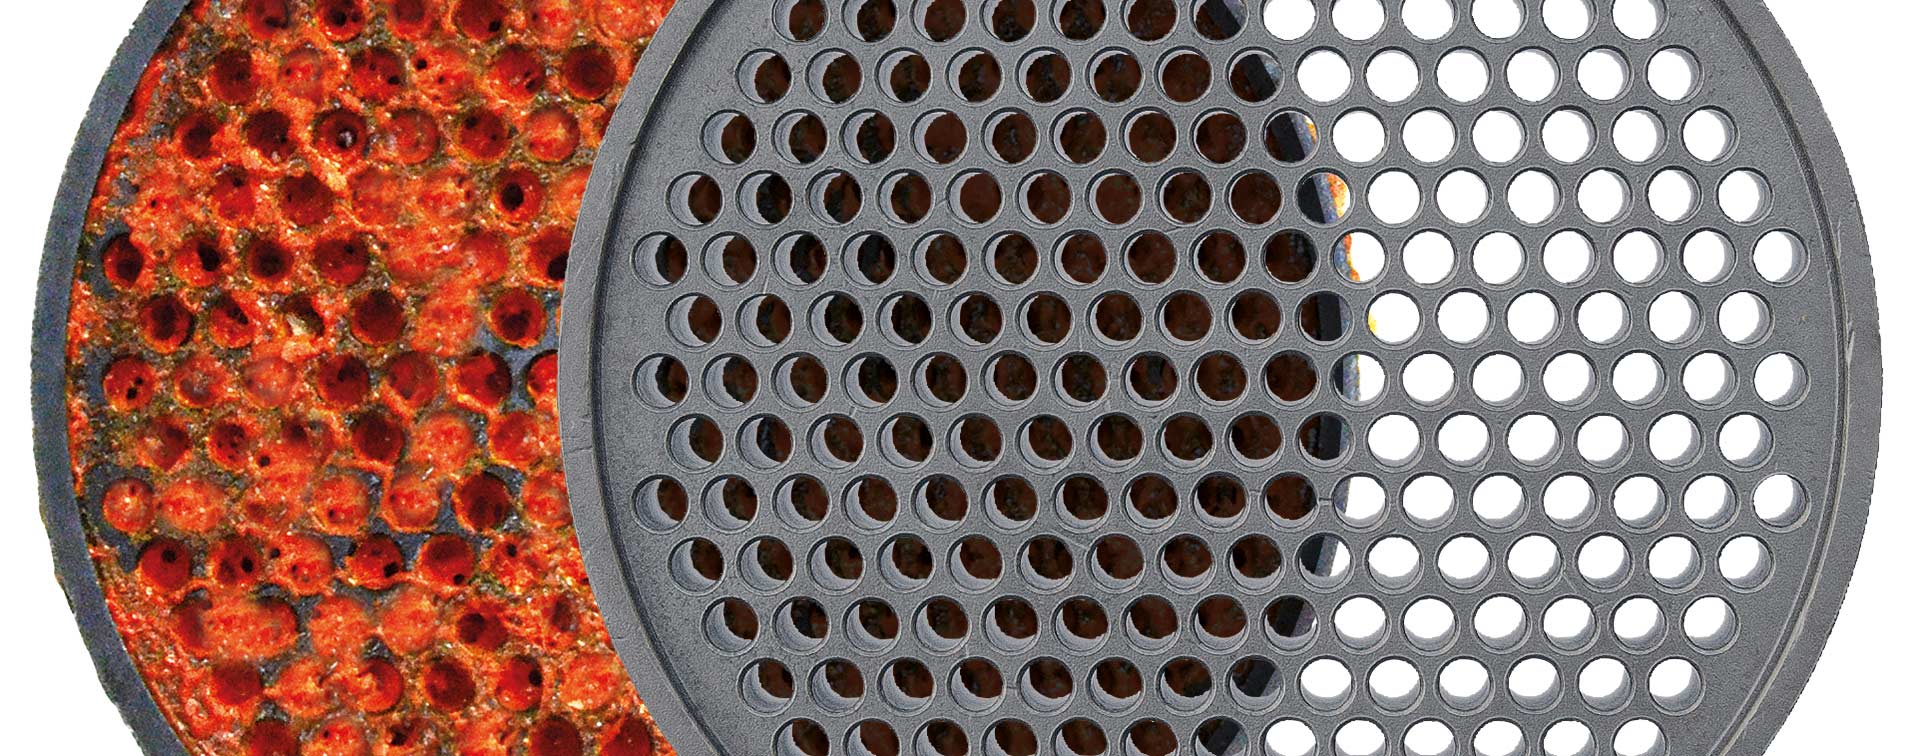
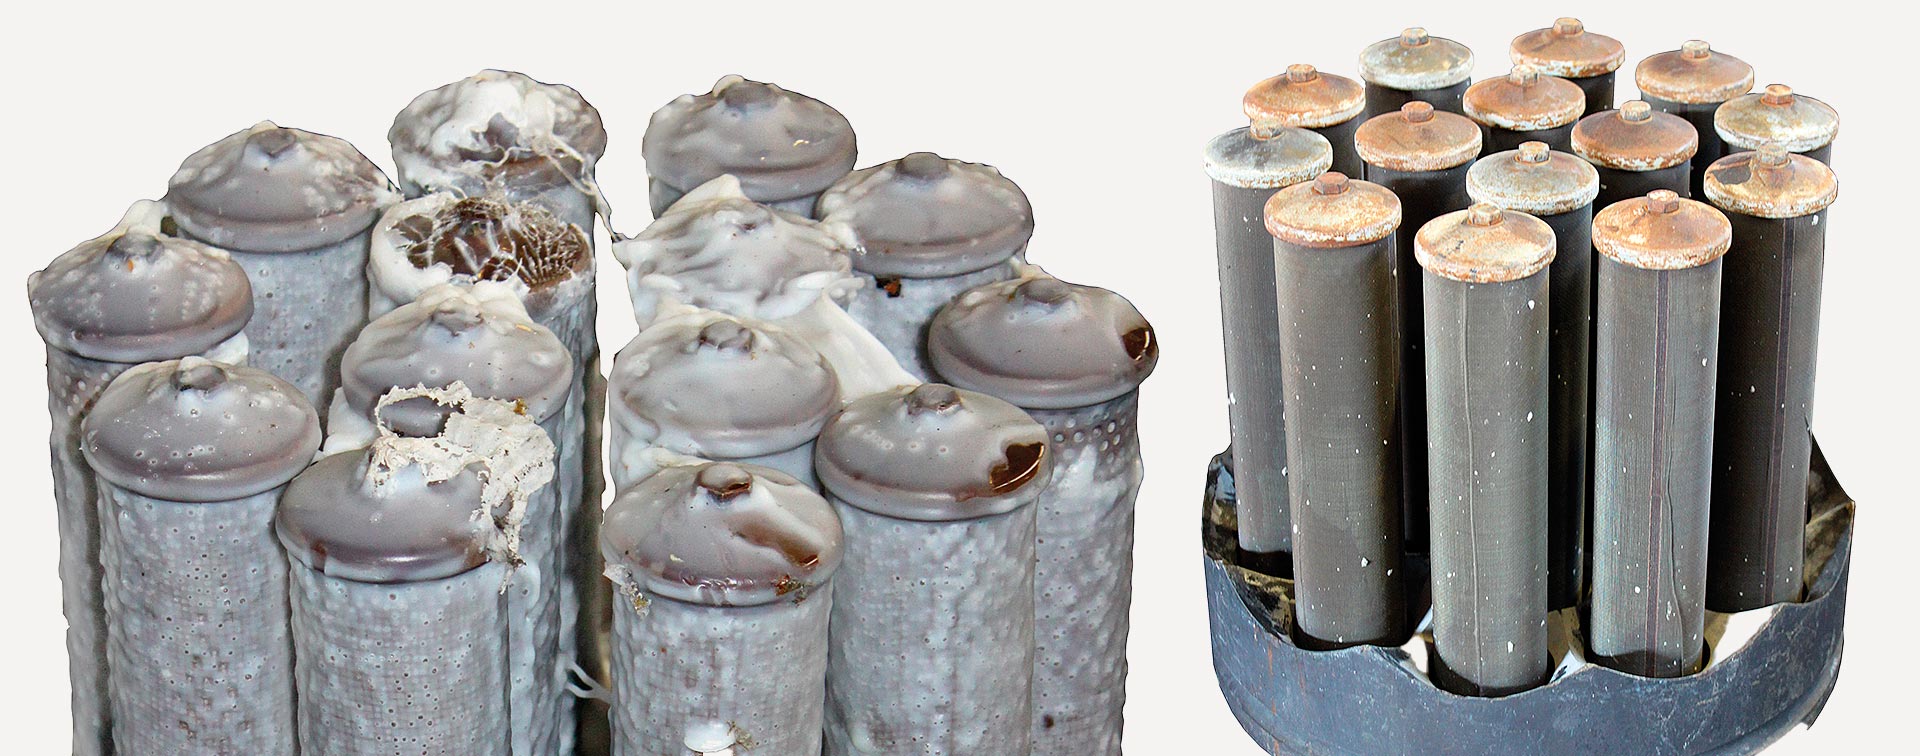
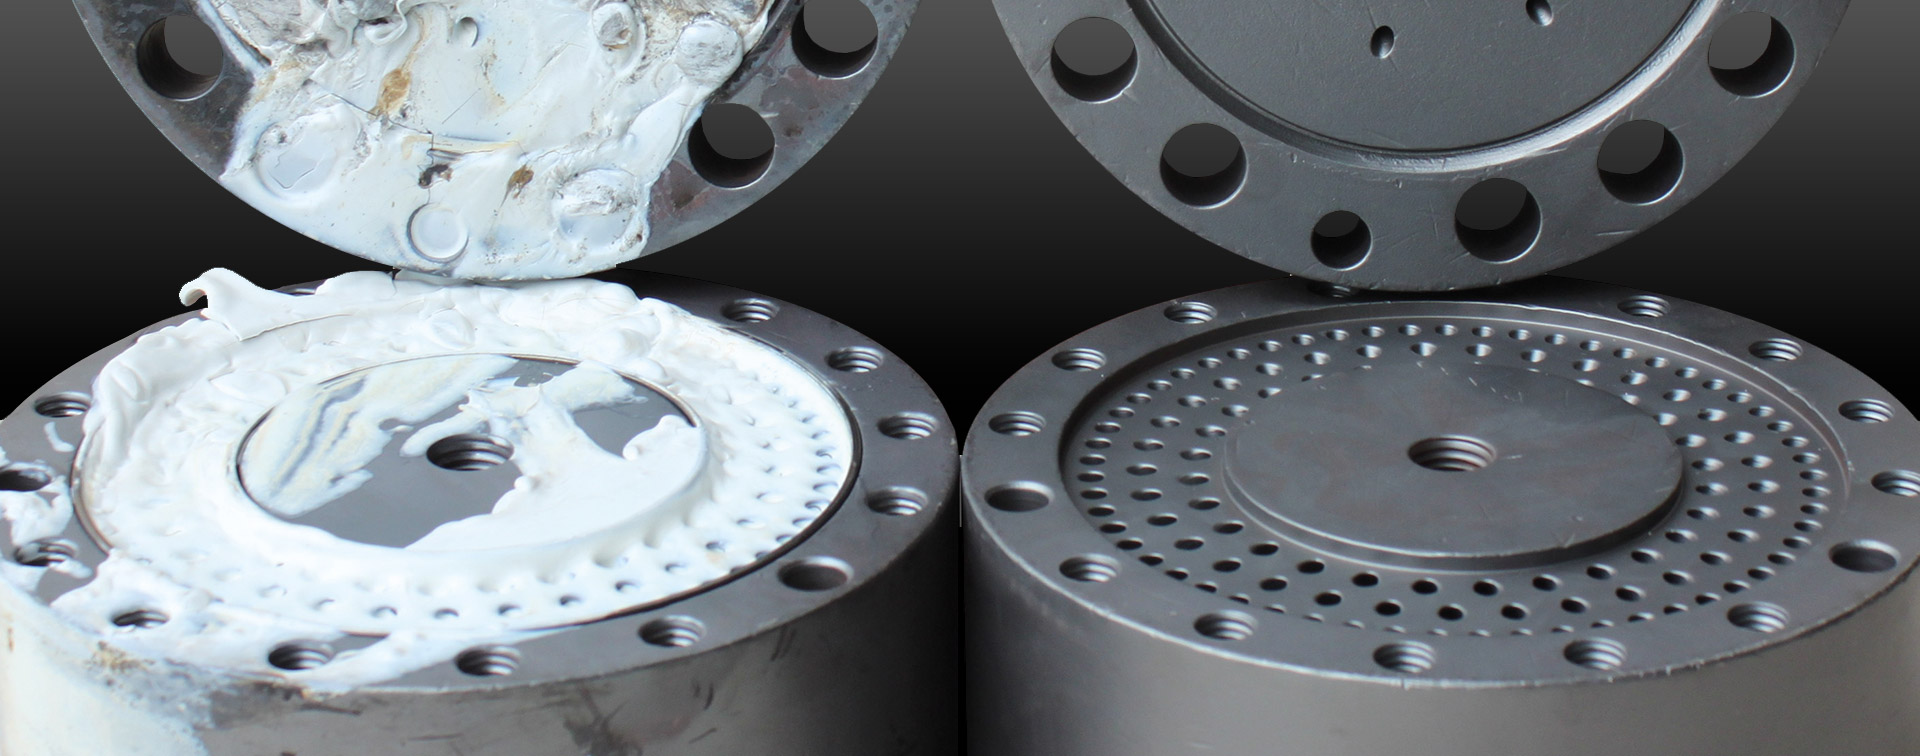
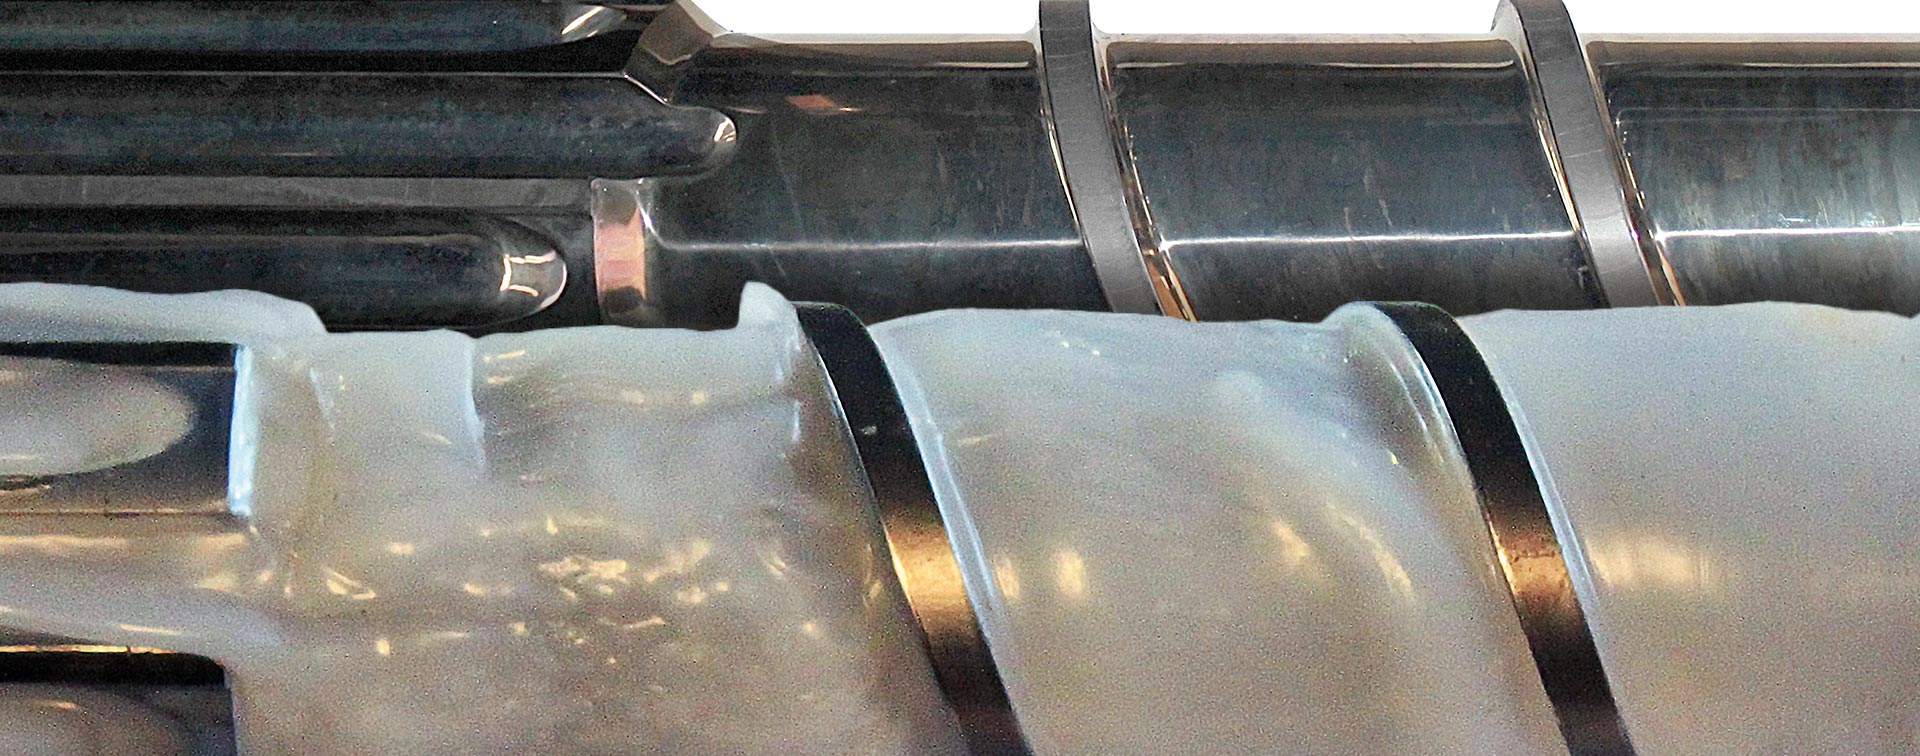
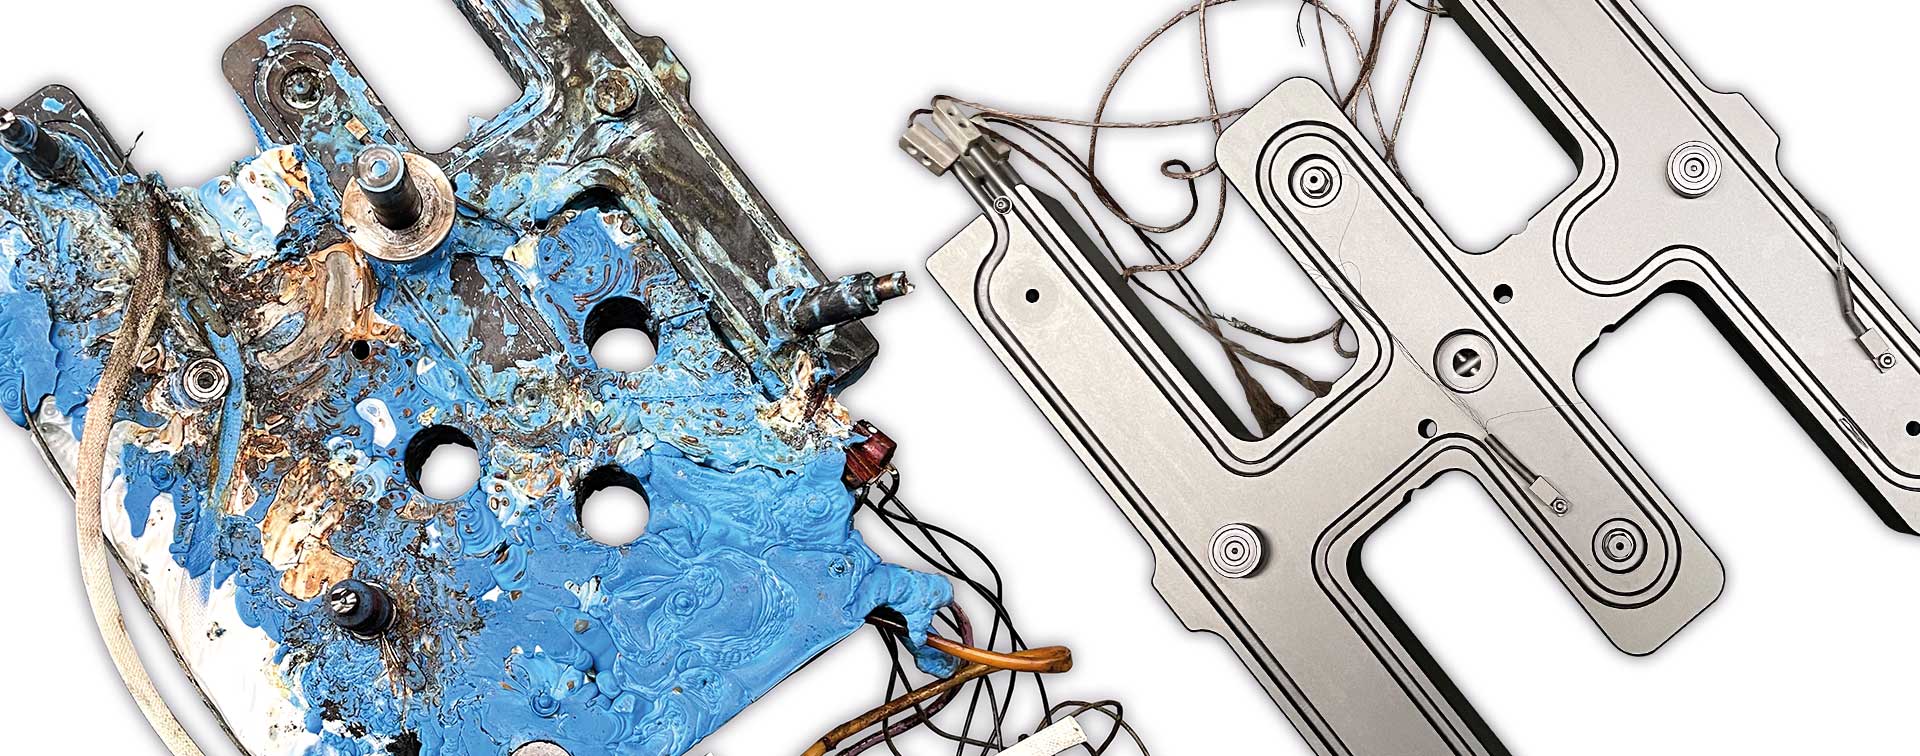
Safely, reliably, and gently remove plastic, polymer, and organic residues—using thermal cleaning processes for extrusion, injection molding, recycling, fiber production, nonwovens, and plastics manufacturing.
Complex tools, filters, nozzles, spinning assemblies, hot-runner components, and extrusion parts must be regularly cleaned of hardened polymer and plastic residues. Thermal cleaning uses controlled pyrolysis and oxidation processes to remove organic residues from heat-resistant metal parts—without mechanical scraping, aggressive chemicals, or uncontrolled burning.
In many industrial processes, polymers, additives, pigments, coatings, or other organic residues adhere to tools and machine parts. This becomes particularly critical in the case of fine bores, internal channels, filter structures, complete spinning packages, as well as hot runners, perforated plates, and extrusion dies.
Mechanical cleaning can damage sensitive surfaces, bores, and capillaries. Chemical cleaning is usually costly, poses risks to the material, or is harmful to the environment. Thermal cleaning offers an industrial alternative when organic residues need to be removed in a controlled, reproducible, and material-friendly manner.
Common challenges:
Thermal cleaning is the controlled removal of organic residues from heat-resistant metal parts using heat. Polymers and plastics are not mechanically scraped off, but rather removed through melting, pyrolysis, thermal decomposition, and subsequent oxidation.
Temperature alone is not the decisive factor. The key factors are controlled process management, the component geometry, the polymer, any additives, the type of residues, exhaust air treatment, and the required post-treatment.
Analyze components and residues or contamination

Select a cleaning method and, if necessary, a post-treatment

If necessary, remove the component and prepare it for cleaning

Thermally decompose the polymer; if necessary, melt it first

Oxidize carbon residues

Post-process and inspect the component

SCHWING Technologies develops, manufactures, and operates high-temperature systems for industrial applications. In the Thermal Cleaning division, the focus is on removing plastic, polymer, and organic residues from metal tools and machine parts.
SCHWING's roots date back to the founding of E. Schwing Verfahrenstechnik KG in 1969.

SCHWING offers solutions for vacuum pyrolysis, fluidized-bed cleaning, and pyrolysis in industrial furnaces—tailored to the specific component, polymer, and cleaning objective.
In addition to its own equipment, SCHWING also offers thermal cleaning as a service—for test cleanings, individual parts, regular cleaning, and outsourcing solutions.
The SCHWING cleaning service cleans more than 250,000 different workpieces each year and reintegrates them into customers' production processes.
At the SCHWING Lab+Tech Center, customers and prospective clients can test processes, conduct test series, and have specific cleaning tasks evaluated from a technical perspective.
There has never been a part so far which we were not able to free completely from attached polymers and inorganic contaminations. Our cleaning systems are suitable for all polymers and plastics:
If "your" material is not listed here, contact our specialists or send us an e-mail.

The method of thermal cleaning is also recommended for the removal of varnishes and other organic coatings of metal parts of all sizes and geometries, for example, of coating tools, electric motors, ink tanks, adhesive pumps or printing suspension gears.

Depending on the component geometry, polymer, degree of contamination, and quality requirements, various thermal cleaning methods may be considered. The selection is always application-specific.

For delicate, complex, and high-quality tools with intricate geometries.

For many small and medium-sized, robust components that require fast, uniform heat transfer.

For large tools, heavy components, and special geometries—depending on the polymer and cleaning objective.
Cleaning Task | Typical Components | Commonly Suitable Process | Note |
|---|---|---|---|
Sensitive filters and complex internal geometries | Filter cartridges, filter discs, laser filters | Vacuum pyrolysis / VACUCLEAN | especially for high-quality or sensitive components |
Small to medium-sized robust components | Nozzles, perforated discs, backflow preventers | Fluidized bed / INNOVACLEAN | short cleaning cycles possible |
Large tools | large hot runners, blow molds, special components | Pyrolysis / MAXICLEAN or VACUCLEAN XXL | depending on size, polymer, and component |
Fiber and nonwoven tools | Spinning nozzles, spinning assemblies, spinning beams | Check on a case-by-case basis | Controlled processes and post-treatment are often relevant |
Recycling filters | Filter cartridges/bundles, filter discs/stacks | VACUCLEAN / VACUCLEAN COMPACT | High quality and service life requirements |
Halogenated Plastics / Polymers | Components containing PVC, PTFE, PVDF, halogen-containing additives | Fluidized bed / INNOVACLEAN | Suitable provided that the component geometry and complete removal of the fluidized bed medium allow it; for fine-pored or very fine structures, consider alternative methods |
Not sure which method is right for you?
Conclusion: For basic cleaning as well as complete cleaning in the field of plastic removal the special SCHWING pyrolysis furnaces and fluidized bed systems are best suited.
Conclusion: this type of cleaning should not be used.
Conclusion: should be used preferably for post-processing of the part being cleaned for partial cleaning.
Conclusion: can be used in post processing for particular contaminants. Otherwise, rather unsuitable.
Conclusion: Post-treatment with ultrasound is the ideal complement for thermal cleaning of small or sensitive components.
Conclusion: not yet economical at present.
All thermal cleaning processes and, if required in post-treatment, other methods for removal of inorganic contaminants.
From plastics processing and recycling to fiber production, packaging, and decoating: Thermal cleaning specifically helps industrial users reliably remove organic residues from metal tools, filters, nozzles, and machine parts. (Applications and industries for thermal cleaning →)
Extrusion, injection molding, hot runners, screws, nozzles, extruder heads
Spinning nozzles, spinning assemblies, spinning beams, spinning pumps, meltblown dies
Film extrusion heads, spiral distributors, wide-slot dies, film extrusion dies
Extrusion dies, perforated plates, polymers, additives, high-performance plastics
Filter cartridges, filter bundles, filter discs, filter stacks, laser filters, filter changers
Painting racks, mounting hooks, coated components, electric motors, stators, rotors
Not sure how to classify your application? — Whether filters, nozzles, spinnerets, hot runners, extrusion dies, or coated metal parts: The ideal thermal cleaning process depends on the component, polymer, residue, and quality requirements.
Thermal cleaning is suitable for numerous heat-resistant metal parts and tools that become contaminated with organic residues during plastics processing, extrusion, fiber production, recycling, or coating processes. Key factors include component geometry, material, polymer, degree of contamination, and desired cleaning quality.
The following component groups illustrate typical applications. The specific process selection should always be technically evaluated.


Can't find your component here? - Many cleaning tasks can only be reliably classified based on geometry, material, polymer, residue, and the desired level of cleanliness. SCHWING is happy to assist you with the technical evaluation of your cleaning requirements.
SCHWING offers a variety of thermal cleaning systems for different components, polymers, batch sizes, and process requirements. The system is selected based on the specific cleaning task.
System | Process Principle | Typical Applications | Further Information |
|---|---|---|---|
VACUCLEAN | Vacuum pyrolysis | gentle cleaning of complex, sensitive, or high-value tools | More about VACUCLEAN → |
VACUCLEAN COMPACT | Compact vacuum pyrolysis | smaller batches, sensitive filters, extrusion tools, nozzles, spinnerets, and complex small parts | Learn more about VACUCLEAN COMPACT → |
INNOVACLEAN | fluidized-bed pyrolysis | rapid cleaning of suitable small and medium-sized components; particularly relevant for halogenated plastics, provided the component geometry allows for the use of the fluidized-bed medium | Learn more about INNOVACLEAN → |
MAXICLEAN | Pyrolysis furnace | large tools, heavy components, and large geometries | More about MAXICLEAN → |
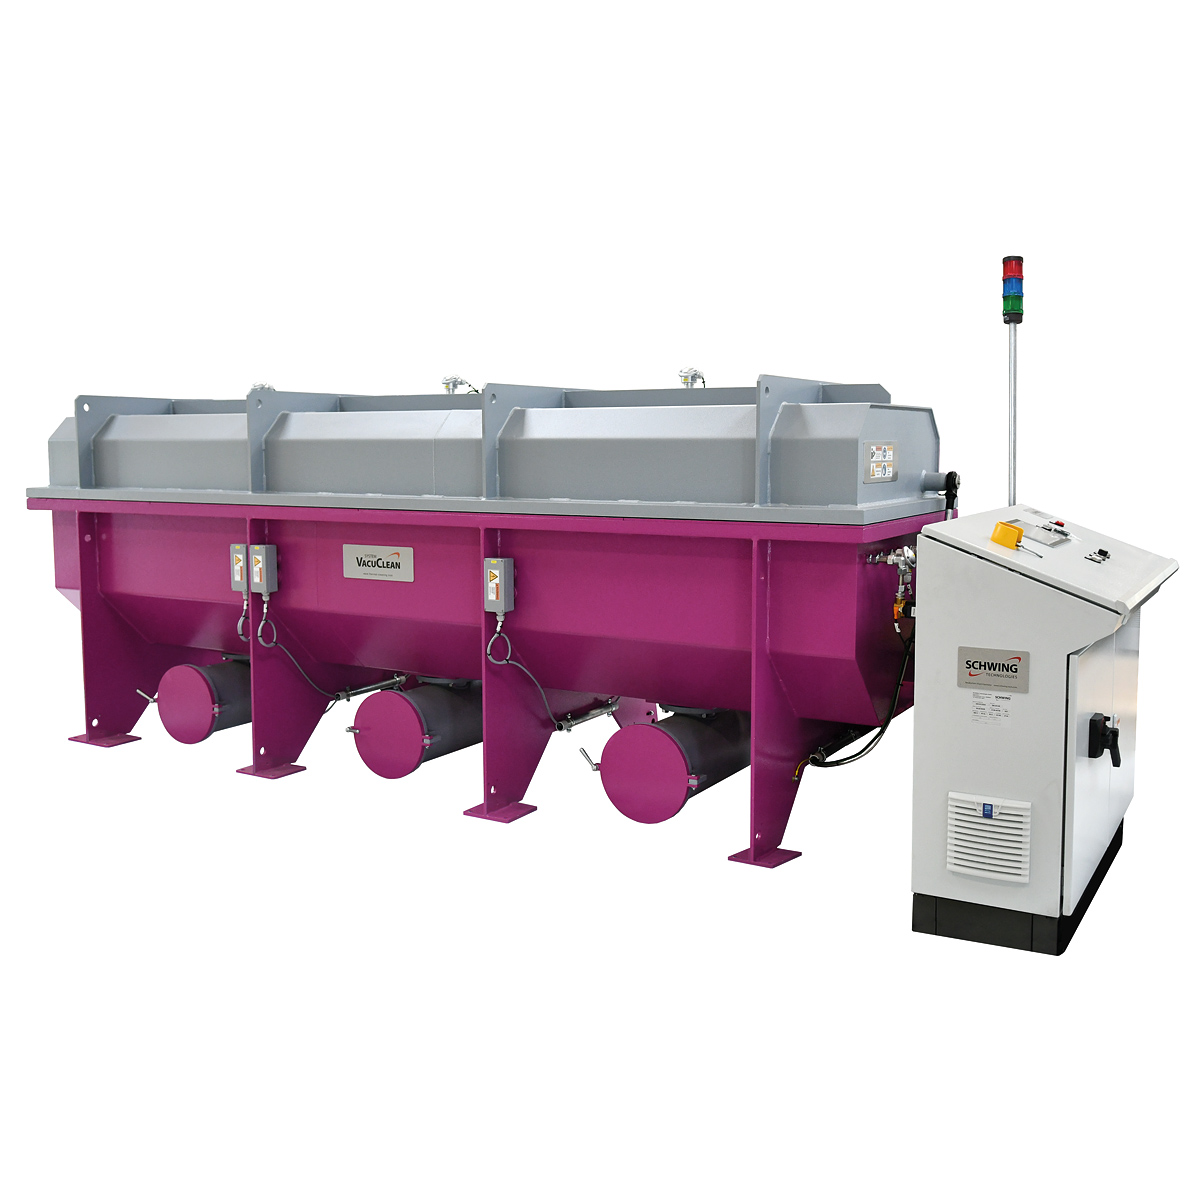


The choice of system always depends on the specific cleaning task. The selection of a process should be technically evaluated, especially in the case of delicate geometries, unknown residues, or halogenated plastics.
Not sure which system is right for your cleaning task?
The right cleaning solution is not determined solely by the component or the polymer. The decisive factor is the combination of cleaning methods, temperature control, exhaust air treatment, post-treatment, quality inspection, and cost-effective process integration. SCHWING therefore views thermal cleaning as a coordinated process chain—from the initial test cleaning to a custom system solution.
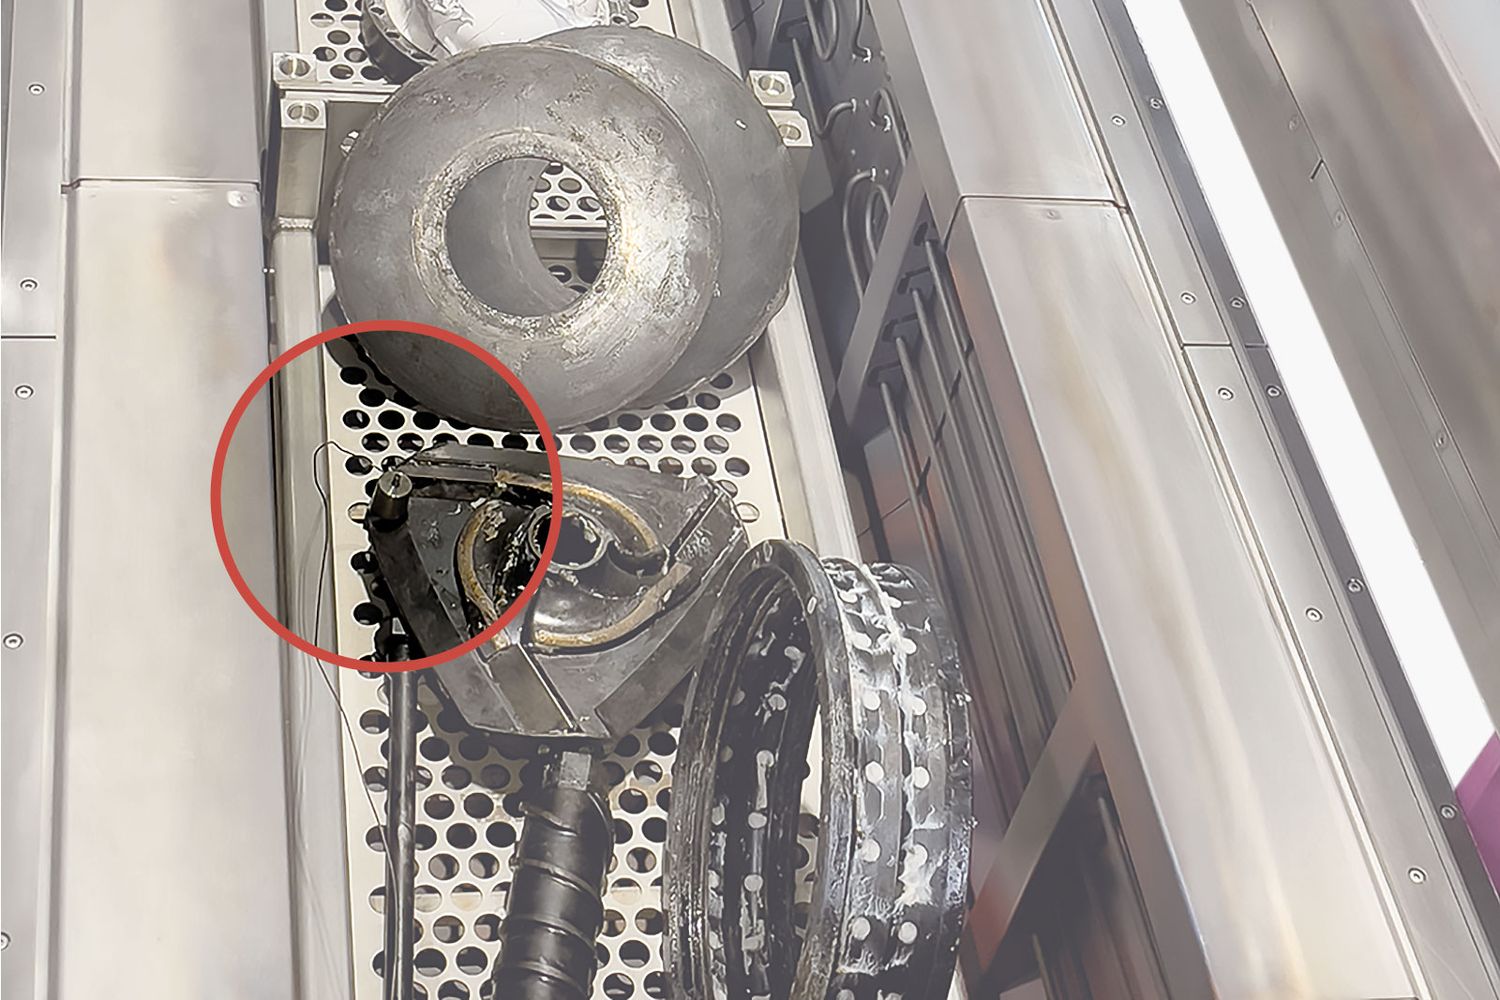

SCHWING evaluates cleaning tasks not from the perspective of a single system, but based on the specific application. Depending on the component, polymer, geometry, and cleaning objective, vacuum pyrolysis, fluidized-bed cleaning, or pyrolysis furnaces may be considered.
SCHWING develops and manufactures thermal cleaning systems and also operates its own cleaning service. As a result, practical cleaning experience, test results, and system expertise are directly incorporated into the technical consulting services.
Customers can have contaminated original parts tested before deciding on a process, service, or in-house facility. This allows them to evaluate the technical suitability of a cleaning solution using actual components and residues.
Thermal cleaning does not end with pyrolysis. Depending on the residue and the component, the process also includes post-treatment, visual inspection, microscopic examination, filter testing, or documentation of the process parameters.
Thermal cleaning involves more than just removing visible plastic or polymer residues. The entire process is critical: controlled temperature management, safe handling of reaction gases, tailored post-treatment, and documented quality control.
Particularly when dealing with high-quality tools, fine capillaries, filter structures, complex internal geometries, or halogenated plastics, this process chain determines whether a cleaned component can be safely, reproducibly, and cost-effectively reused. (Frequently Asked Questions About Thermal Cleaning →)
Thermal cleaning must be conducted in such a way that organic residues are reliably decomposed without subjecting the items being cleaned to unnecessary thermal stress. Depending on the process, polymer, component geometry, and cleaning objective, different temperature profiles and process phases are used.
For particularly sensitive tools, controlled process management that minimizes damage to the components is crucial—for example, in the case of spinnerets, laser filters, filter structures, or complex extrusion dies.
The thermal decomposition of plastics, additives, paints, or other organic residues can produce gaseous reaction products. These must be safely removed, treated, or captured.
This is particularly important for halogenated plastics, as their decomposition can produce aggressive or corrosive decomposition products. INNOVACLEAN is particularly well-suited for such applications and for components whose geometry allows for the use of the fluidized-bed medium.
Not all residues are removed solely by pyrolysis, vacuum decomposition, or fluidized-bed processes. Fillers, color pigments, talc, glass fibers, additives, or inorganic byproducts may require specific post-treatment after thermal cleaning.
Depending on the component and type of contamination, methods such as ultrasonics, high-pressure water jets, compressed air, or blasting may be used. The goal is not only to achieve a visually clean surface but also to restore the functionality of channels, pores, capillaries, and surfaces.
For industrial users, it’s not just about a component looking clean. What matters most is that the cleaning process is traceable, reproducible, and quality-assured.
Depending on the application, process data can be documented, components can be visually inspected, and sensitive structures can be checked using appropriate testing methods—such as the capillaries of spinnerets or the condition of filter systems.
Details:
Thermal cleaning must be conducted in such a way that organic residues are reliably decomposed without subjecting the items being cleaned to unnecessary thermal stress. Depending on the process, polymer, component geometry, and cleaning objective, different temperature profiles and process phases are used.
For particularly sensitive tools, controlled process management that minimizes damage to the components is crucial—for example, in the case of spinnerets, laser filters, filter structures, or complex extrusion dies.
The thermal decomposition of plastics, additives, paints, or other organic residues can produce gaseous reaction products. These must be safely removed, treated, or captured.
This is particularly important for halogenated plastics, as their decomposition can produce aggressive or corrosive byproducts. INNOVACLEAN fluidized-bed technology is especially well-suited for such applications.
Not all residues are removed solely by pyrolysis, vacuum decomposition, or fluidized-bed processes. Fillers, color pigments, talc, glass fibers, additives, or inorganic byproducts may require specific post-treatment after thermal cleaning.
Depending on the component and type of contamination, methods such as ultrasonics, high-pressure water jets, compressed air, or blasting may be used. The goal is not only to achieve a visually clean surface but also to restore the functionality of channels, pores, capillaries, and surfaces.
For industrial users, it’s not just about a component looking clean. What matters most is that the cleaning process is traceable, reproducible, and quality-assured.
Depending on the application, process data can be documented, components can be visually inspected, and sensitive structures can be checked using appropriate testing methods—such as the capillaries of spinnerets or the condition of filter systems.
Would you like to know what post-treatment is required for your component?
Have the cleaning task evaluated from a technical perspective→
Not every cleaning task requires a capital investment in equipment. Depending on the frequency, the value of the components, the production situation, and technical uncertainties, it may make sense to start with a cleaning service, a trial cleaning, or a pilot design for an in-house system.

Suitable for occasional cleaning tasks, capacity bottlenecks, external capacity, or companies without their own cleaning facilities.
• Individual components or small production runs•
Acute cleaning bottlenecks•
External
high-quality cleaning• Evaluation prior to a future investment

Recommended for new components, unknown polymers, critical geometries, or before making an investment decision.
• Unknown
residues • Sensitive component
geometries • New production
processes • Comparison of different cleaning methods
Discuss a test cleaning →

Suitable for regular cleaning cycles, high-value tools, short maintenance windows, and strategic process integration.
• High, regular cleaning
requirements • Sensitive or valuable
tools • Short downtime
periods • International production sites
Would you like to figure out what the next logical step is?
For an initial technical assessment, just a few pieces of information are key. Based on this information, we can determine whether our cleaning service, a trial cleaning, or your own thermal cleaning system is the most sensible next step.
Tell us the name of your component, the type of residue adhering to it, and your goal. SCHWING will review your inquiry and contact you with a technical assessment.
The following answers provide an initial guide to the thermal cleaning of metal parts and tools. The solution best suited to a particular case depends on the component, material, residue, polymer, geometry, and desired level of cleanliness.
Thermal cleaning is an industrial process for removing organic residues from heat-resistant metal parts and tools. Plastics, polymers, paints, or other organic deposits are heated, melted, decomposed, or oxidized in a controlled manner. The goal is to achieve reproducible cleaning without mechanical scraping or aggressive manual processing.
Typical parts include filter cartridges, filter discs, laser filters, spinning nozzles, spinning assemblies, extruder screws, screw elements, film blowing heads, hot runners, injection nozzles, perforated plates, pelletizing dies, and coated metal parts. It is crucial that the component be suitable for the required temperatures. Its specific suitability should always be verified based on the material, geometry, and residue.
In particular, organic residues such as plastics, polymers, additives, paints, varnishes, resins, rubber, or similar deposits can be removed. In the case of plastics containing fillers, pigments, glass fibers, or mineral components, inorganic residues may remain after thermal treatment. If necessary, these are removed through a tailored post-treatment process.
The most important processes include vacuum pyrolysis, fluidized-bed pyrolysis, and pyrolysis in an industrial furnace. Vacuum pyrolysis is particularly suitable for complex or delicate tools. Fluidized-bed pyrolysis is suitable for many small and medium-sized components. Pyrolysis furnaces are frequently used for large tools, heavy components, or larger batches.
The appropriate process depends on several factors: part geometry, material, polymer, degree of contamination, amount of residue, part size, desired cleaning quality, and any potential post-treatment. Therefore, the selection should not be based solely on industry or part type. The specific cleaning task is the decisive factor.
Yes, depending on the design, materials, and cleaning process, even complex or multi-part tools can be thermally cleaned. For assembled components, it is necessary to verify that all components are sufficiently heat-resistant and that the areas to be cleaned can be accessed. Temperature-sensitive or non-metallic inserts may need to be removed before cleaning. For some tools—such as spinning packages—thermal pretreatment can first make disassembly possible; the individual components are then cleaned thoroughly.
Follow-up treatment is required if, after thermal cleaning, inorganic residues, fillers, pigments, glass fibers, talc, or other particles remain in or on the component. Depending on the application, ultrasonic cleaning, high-pressure water, compressed air, blasting, or special testing methods are used. The goal is not only to achieve a clean surface but also to restore the component’s functionality.
A few details are usually sufficient for an initial assessment: Which component needs to be cleaned, what type of plastic or residue is adhering to it, how large and heavy is the part, and what is the goal? Photos, drawings, data sheets, or information about the current cleaning method are also helpful. Further technical details can then be clarified directly.
For more answers to frequently asked questions, see the detailed FAQ section on thermal cleaning: View the detailed FAQ→
Whether you need a cleaning service, a trial cleaning, or your own system:
SCHWING can help you select the right thermal cleaning process for your components, polymers, and production requirements.
back-to-top